Processing & Quality Infrastructure
Ratona Bee operates with dedicated honey processing, quality control, and storage infrastructure to ensure every batch of honey meets international standards before reaching our domestic and global business partners.
Honey Processing Unit
Our processing unit utilizes food-grade stainless steel (SUS304) tanks and multi-stage fine mesh filtration. We apply gentle, low-temperature handling (under 40°C) to remove natural beeswax particles, hive fragments, and organic debris without degrading delicate pollen, diastase enzyme activity, or antioxidant flavonoids.
Quality Control & In-House Testing Laboratory
Every incoming batch from our beekeeper network undergoes systematic quarantine and testing. Our in-house QC station verifies moisture content via calibrated digital refractometers, optical Brix density. We partner with accredited ISO/IEC 17025 laboratories for comprehensive C4 sugar isotope, HMF, and antibiotic residue certifications.
Cleanroom Storage & Climate-Managed Warehousing
Processed honey is housed in clean, climate-controlled warehousing shielded from direct sunlight and ambient humidity spikes. Strict storage systems ensure full traceability and product freshness from farm to shipment.
Packaging & Export Dispatch Terminal
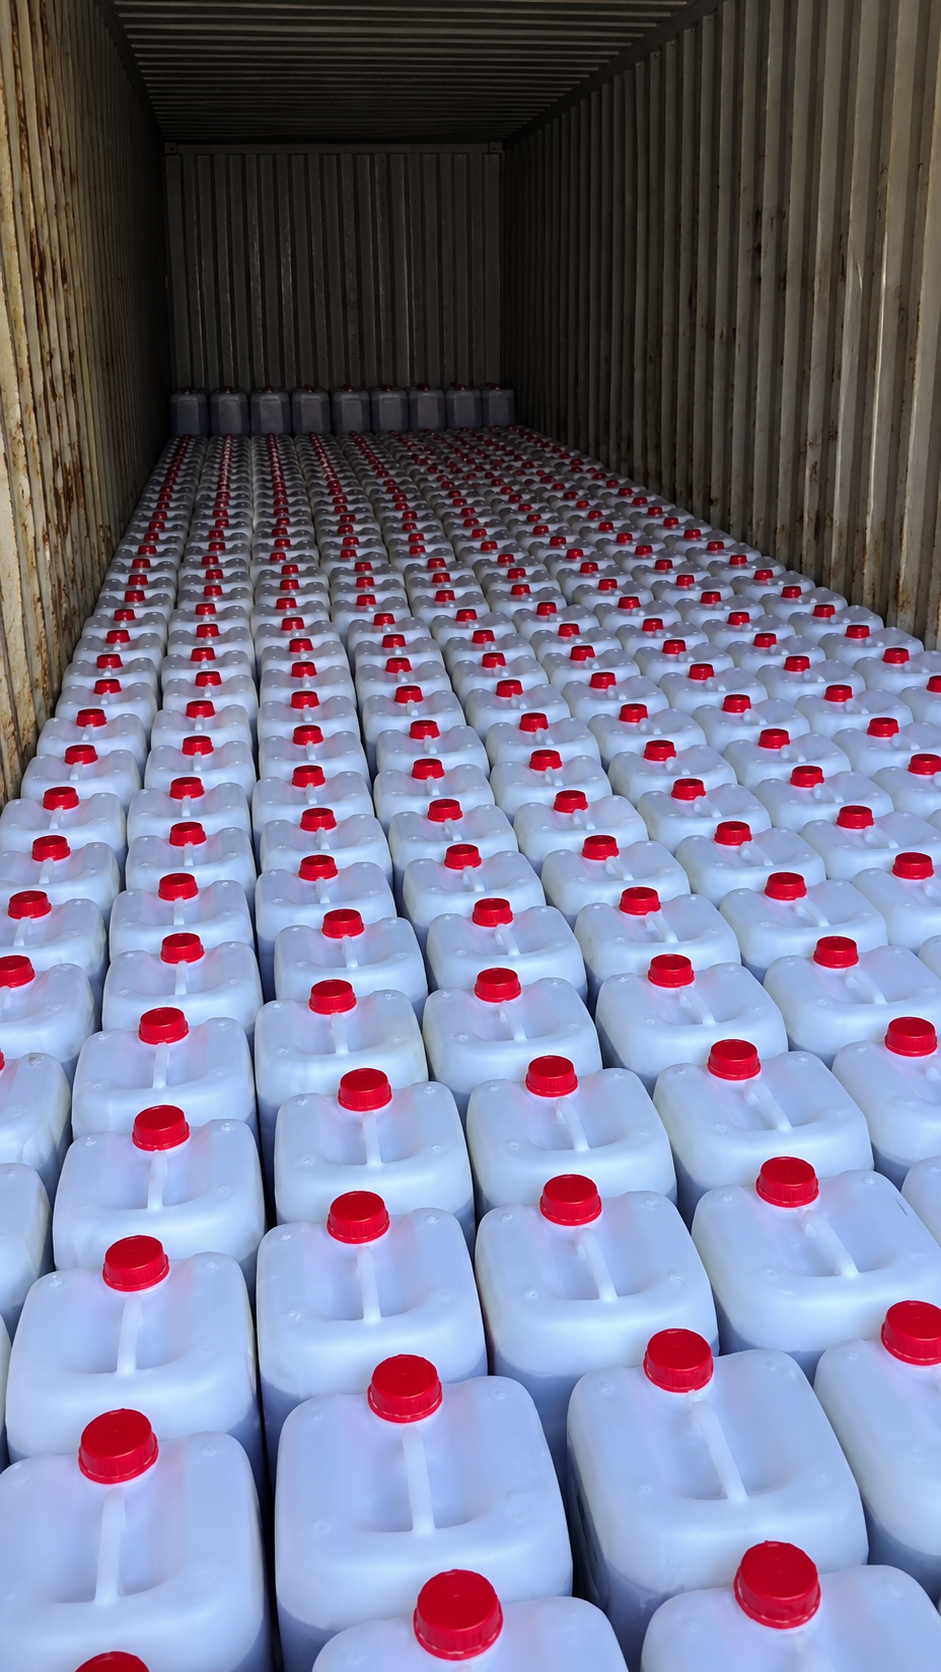
Our filling and packaging lines accommodate diverse market formats: automated retail glass and squeezable PET jars for commercial consumer brands, 25kg–30kg food-grade UN-rated jerrycans, and heavy-duty 290kg–300kg epoxy-coated steel or high-density polyethylene (HDPE) drums for international shipping containers.
Our Operational Benchmarks
Moisture Control (18–19%)
Managed gently without heat damage to prevent fermentation during ocean transit and maintain Codex Alimentarius standards.
Zero Added Sugars Guarantee
100% authentic unadulterated honey verified against C4 corn syrup, rice syrup, and invert sugar compounds.
Food-Grade Contact Materials
All processing piping, valves, and bulk transport drums are certified food-contact compliant (SUS304 / Virgin HDPE).
Full Supply Chain Traceability
Every dispatch lot carries laboratory Certificate of Analysis (CoA), and export manifests.
Looking for a Verified Honey Supplier?
Schedule a facility inspection or request official analytical reports for your business partnership requirements.